 EN

why-choose-nbr-rubber-hose-for-industrial-applications, why-choose-nbr-rubber-hose-for-industrial-applications, /news
EN
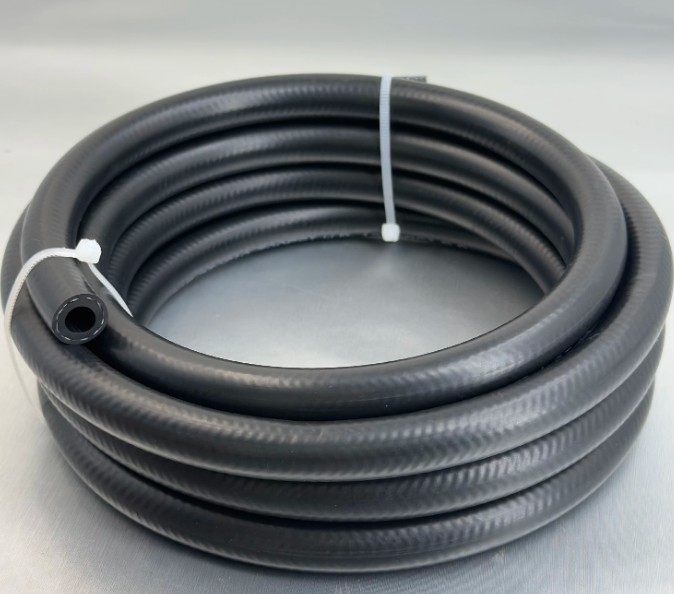
Industrial operations depend on reliable fluid transfer systems, and the choice of hose material directly impacts performance, safety, and operational costs. NBR rubber hose has become the industry standard for applications requiring exceptional durability and chemical resistance. Unlike generic rubber alternatives, nitrile rubber tubing delivers consistent performance across demanding environments where oil exposure, temperature fluctuations, and mechanical stress are constant challenges.
Understanding why synthetic rubber hose applications favor nitrile compounds requires examining the material science behind fluid transfer systems. Oil resistant rubber hoses manufactured from NBR provide superior protection against hydrocarbon degradation, thermal aging, and mechanical fatigue. This makes them ideal for automotive fuel lines, hydraulic systems, industrial machinery, and chemical processing equipment where failure carries significant operational and safety consequences.
NBR rubber hose excels where petroleum-based fluids are present. Nitrile rubber tubing resists swelling, cracking, and degradation when exposed to diesel, gasoline, hydraulic oils, and synthetic fuels. Traditional rubber compounds absorb these fluids, causing dimensional changes that compromise seal integrity and system performance. The polarity of nitrile rubber creates molecular bonds that repel hydrocarbon molecules, maintaining hose dimensions and flexibility throughout service life.
Oil resistant rubber hoses using NBR formulations maintain their mechanical properties across extended temperature ranges. At 40 degrees Celsius, nitrile rubber tubing maintains full flexibility and grip strength. Even at elevated operating temperatures reaching 100 degrees Celsius, synthetic rubber hose applications using NBR show minimal performance degradation. This thermal stability prevents the brittleness that develops in natural rubber or lower-grade synthetic alternatives.
Investing in NBR rubber hose reduces total system ownership costs despite higher initial material expenses. Oil resistant rubber hoses crafted from nitrile compounds resist premature failure, reducing replacement frequency and associated downtime. Industrial operations benefit from fewer emergency maintenance calls and reduced inventory requirements for spare hoses. Nitrile rubber tubing typically delivers 5 to 7 years of reliable service in standard applications, with some systems exceeding 10 years under optimal conditions.
The automotive industry relies heavily on synthetic rubber hose applications using NBR for fuel delivery, vapor lines, and hydraulic brake systems. NBR rubber hose meets stringent OEM specifications for fuel system compatibility, pressure ratings, and temperature cycling durability. Nitrile rubber tubing withstands the rapid temperature changes experienced in engine compartments, from below-freezing winter starts to high-heat summer operation. Oil resistant rubber hoses protect against fuel contamination and vapor permeation, critical factors in maintaining fuel system integrity and vehicle performance.
Heavy machinery operators depend on oil resistant rubber hoses for hydraulic power transmission in construction equipment, agricultural machinery, and manufacturing facilities. NBR rubber hose handles high-pressure hydraulic fluid with consistent performance, preventing leaks that waste energy and create hazardous spills. Synthetic rubber hose applications in industrial settings benefit from nitrile's resistance to water absorption and bacterial growth, issues that compromise performance in natural rubber alternatives. Nitrile rubber tubing remains dimensionally stable even when subjected to thousands of pressure cycles, maintaining seal effectiveness and system efficiency.
Chemical plants and processing facilities often require NBR rubber hose for transferring various petroleum derivatives and industrial oils. Oil resistant rubber hoses provide reliable containment for aggressive fluids while maintaining FDA and food-grade compliance for certain applications. Synthetic rubber hose applications extend beyond traditional hydraulics into specialized domains including food processing equipment, pharmaceutical manufacturing, and water treatment systems. Nitrile rubber tubing's versatility makes it the default choice when multiple chemical compatibility requirements must be met simultaneously.
NBR rubber hose delivers consistent pressure ratings suitable for both low-pressure transfer lines and high-pressure hydraulic systems. Nitrile rubber tubing maintains structural integrity under pressures exceeding 300 bar in reinforced configurations, far exceeding the capabilities of unreinforced rubber alternatives. The tensile strength of oil resistant rubber hoses ensures resistance to abrasion and physical damage during installation and operation. Synthetic rubber hose applications benefit from predictable burst pressures and reliable safety margins, enabling engineers to design systems with confidence in long-term performance.
Temperature extremes pose challenges for lesser-quality rubber compounds, but NBR rubber hose maintains functionality from minus 40 to plus 100 degrees Celsius in standard formulations. Nitrile rubber tubing resists ozone cracking, a common failure mode in outdoor or UV-exposed applications. Oil resistant rubber hoses stored in warehouses or used in industrial environments resist environmental degradation better than natural rubber alternatives. Synthetic rubber hose applications benefit from superior weathering properties, allowing multi-year storage without significant performance loss.
NBR rubber hose outperforms natural rubber in oil resistance, temperature stability, and ozone protection. Nitrile rubber tubing resists petroleum fluid absorption that causes natural rubber to swell and fail. Oil resistant rubber hoses manufactured from synthetic rubber compounds maintain dimensional stability and mechanical properties under conditions that degrade natural rubber. Synthetic rubber hose applications require the chemical resistance and thermal consistency that only nitrile provides for critical industrial systems.
Certain NBR rubber hose formulations meet FDA compliance requirements for food-grade applications, though not all nitrile compounds qualify. Oil resistant rubber hoses must be specifically manufactured and certified for food contact to ensure safety and regulatory compliance. Synthetic rubber hose applications in food processing facilities require documented NSF certification and material purity validation. Always verify that your specific nitrile rubber tubing meets local food safety regulations before deployment in beverage or food processing systems.
NBR rubber hose requires storage in cool, dry environments away from direct sunlight and ozone sources to preserve material properties. Nitrile rubber tubing should be stored at temperatures between 15 and 25 degrees Celsius with moderate humidity levels. Oil resistant rubber hoses remain stable for years when protected from extreme temperature fluctuations and UV exposure. Synthetic rubber hose applications benefit from proper inventory rotation using first-in, first-out practices to ensure consistent quality and eliminate aged stock.
